


Results 1 to 13 of 13
-
02-23-2011 #1

 Registered User
- Join Date
- Sep 2010
- Location
- Beach Park IL
- Posts
- 3,054

adjustable link brackets - How close are your holes?
When making brackets for link brackets (in this case the front upper mount on a 3link) how close together can you put the holes? It seems to me 1" (on center) spacing with a 9/16" bolt would be safe but.... I keep seeing these pre made brackets for the roundy round guys and they are basically slots. So if I drilled 9/16" holes on 5/8" centers would that live?
Donny
-
02-23-2011 #2

 Registered User
- Join Date
- Apr 2009
- Location
- san diego
- Posts
- 5,101
Check out my build thread I just posted pictures of my arc slotted UCA bracket for my 3-link
My build thread: https://www.pro-touring.com/showthre...ing&highlight=
The mustang build thread: https://www.pro-touring.com/showthre...el)&highlight=
-
02-23-2011 #3
Registered User
- Join Date
- Jan 2010
- Location
- Elk River, MN
- Posts
- 676
Nothing wrong with a slotted bracket, or one with the holes nearly touching. Reason being is that the vertical force vector on your link bolts will never be very high. This is of course assuming that you don't have 3000 horsepower, 100% traction and a ton of antisquat ;)
-mattMatt Peterson 84 Monte Carlo - Sold :( | 99 Corvette Racecar | 2001 Z06 Daily Driver
https://www.pro-touring.com/showthre...ng-Bertha-Back
http://ls1tech.com/forums/conversions-hybrids/1499192-84-monte-5-3-build.html
https://www.pro-touring.com/threads/...rvette-Racecar
-
02-24-2011 #4
Registered User
- Join Date
- Sep 2010
- Location
- Beach Park IL
- Posts
- 3,054
Cool, the only reason I was thinking holes that are really close together is that it would be easier to know how much adjustment I am making....if that makes sense. With a slotted hole I would have to measure any adjustment I made....I'm too lazy for that.
Bryce, is that 3/16" material? I tried to look through the build thread but I am supposed to be working and couldn't find with all the "atta boy's" you got.
I think it will be fine then, I have 2600 horsepower with top fuel slicks but only 60% anti squat. :D
-
02-24-2011 #5
Registered User
- Join Date
- Jan 2010
- Location
- Elk River, MN
- Posts
- 676
Have you considered scalloped holes? Basically where you have a bunch of holes, but the edges overlap. So, it's a slot, but you have to remove the bolt to change holes. This would allow you finer adjustment, without having to guess or measure like with a smoothe slot. The upper A-arms on our Lefthander were like this for adjusting anti-dive, I've never seen it on a trailing arm mount but I see no reason it wouldn't work for your application.
According to my high precision force vector analyzator, with 2600hp and 60% A/S, slots will be fine ;)
-mattMatt Peterson 84 Monte Carlo - Sold :( | 99 Corvette Racecar | 2001 Z06 Daily Driver
https://www.pro-touring.com/showthre...ng-Bertha-Back
http://ls1tech.com/forums/conversions-hybrids/1499192-84-monte-5-3-build.html
https://www.pro-touring.com/threads/...rvette-Racecar
02-24-2011 #6
Registered User
- Join Date
- Apr 2009
- Location
- san diego
- Posts
- 5,101
I am running 1/8" material, after running calculations I determined this is a sufficient thickness for my setup. Originally Posted by dontlifttoshift
 My build thread: https://www.pro-touring.com/showthre...ing&highlight=
The mustang build thread: https://www.pro-touring.com/showthre...el)&highlight=
02-24-2011 #7
Registered User
- Join Date
- Sep 2010
- Location
- Beach Park IL
- Posts
- 3,054
Scalloped holes are exactly what I was thinking, I just didn't know how to put it into words. I think that will work great for what I am doing I will be able to adjust AS% from about 40 to to 100 10% at a time then.
Thanks
Donny
02-24-2011 #8
Registered User
- Join Date
- Jan 2010
- Location
- Elk River, MN
- Posts
- 676
You have someone to make them for you? If not let me know and I could help you get some laser-cut pieces made at work, it's what I does

-mattMatt Peterson 84 Monte Carlo - Sold :( | 99 Corvette Racecar | 2001 Z06 Daily Driver
https://www.pro-touring.com/showthre...ng-Bertha-Back
http://ls1tech.com/forums/conversions-hybrids/1499192-84-monte-5-3-build.html
https://www.pro-touring.com/threads/...rvette-Racecar
02-24-2011 #9
Registered User
- Join Date
- Sep 2010
- Location
- Beach Park IL
- Posts
- 3,054
Man I sure wish you closer! I am fighting with laser shops right now, they both said no problem for prototype stuff and then I send files and no one replies to my emails. For little stuff Ill keep you in mind for sure but the stuff I am trying to get done is about 3 foot across and the shipping would
be stupid I'm sure.
There now I derailed my own thread.
02-24-2011 #10 Registered User
- Join Date
- Nov 2008
- Location
- So. Cal.
- Posts
- 1,240
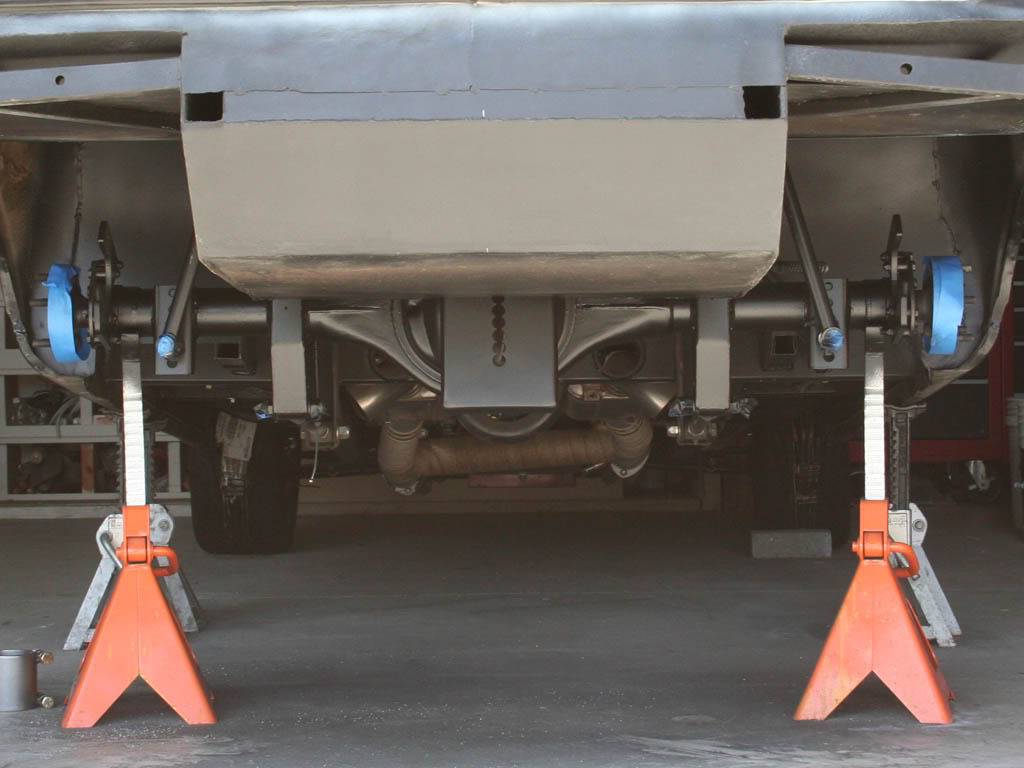
I made a scalloped slot for my watts link. Its nice to have some metal left VS a smooth slot so the bolt will not move vertically.
How much metal (hole spacing) will prolly be determined on how thick the plates are and what the loading is. Say for 3/16" plate which is common suspension material, and for a not heavily loaded piece (in the vertical plane) a slight nib of a 1/16" will work to locate the bolt and keep it from deforming. And give you the maximum adjustability within a short slot. And with the addition of some heavy 1/16" grade eight washers it will help to support the entire fitment.
Oh by the way, I like that definition for that type of slot.
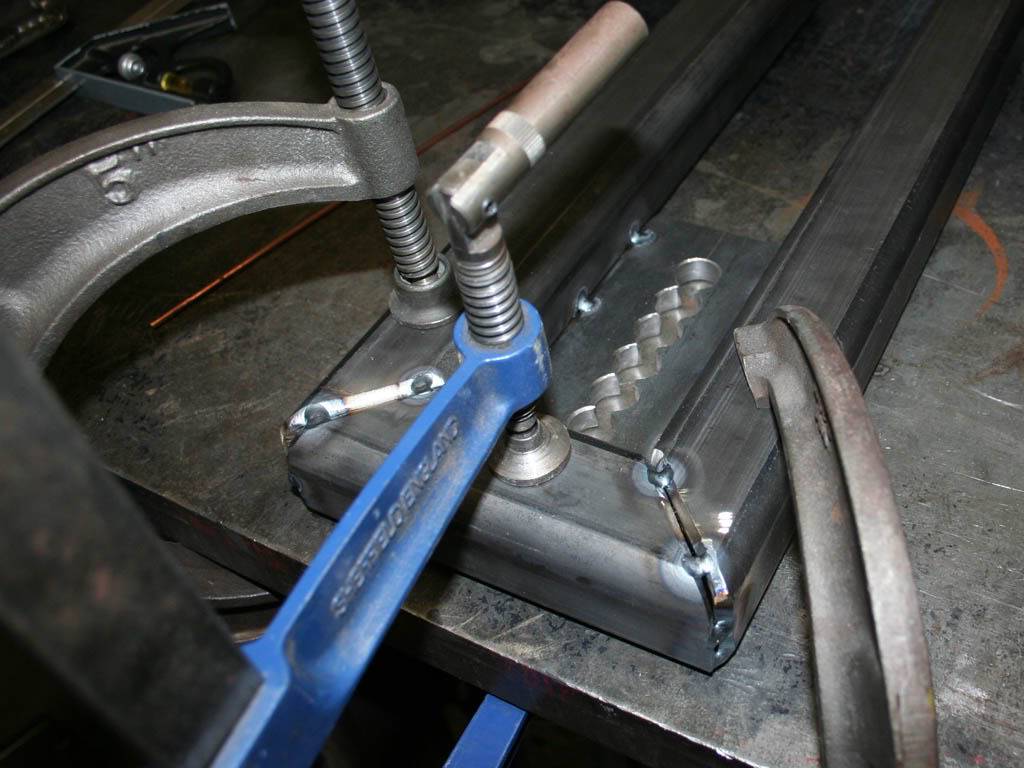
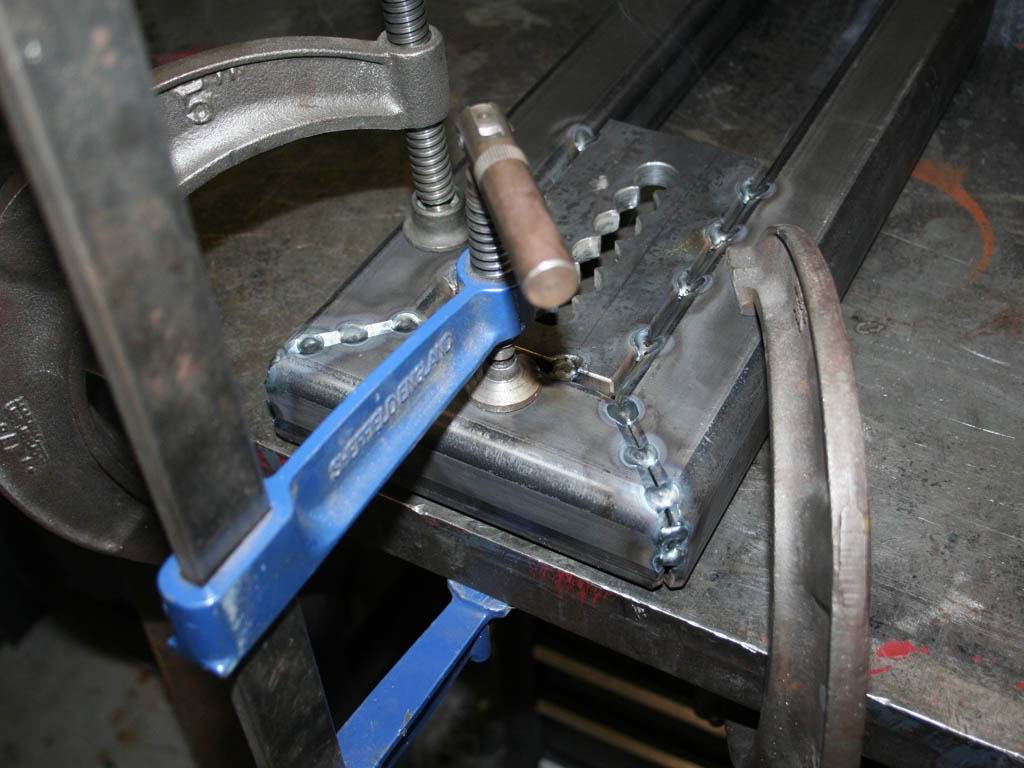
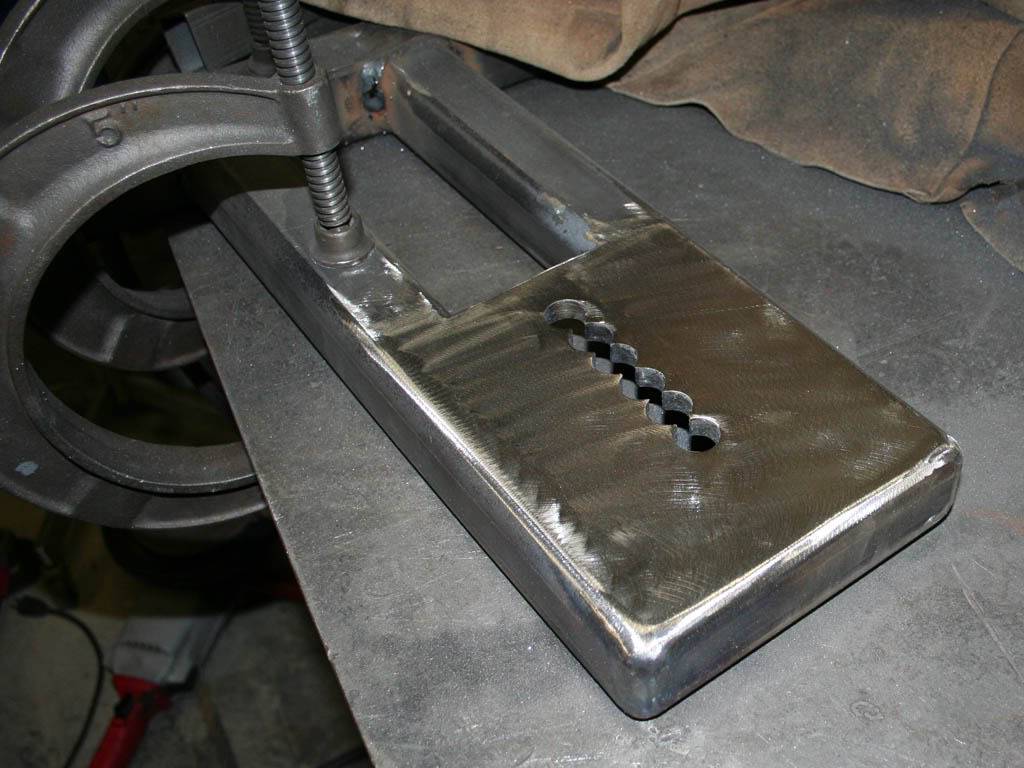
Here is my drilled and reamed scalloped slot, 3/4" holes in 1/2" plate.. JR
 What I write is opinion, none of it is factual. 2010
Even though I'm conscious it doesn't mean I'm coherent. 2011
I'm getting better with age. Best thing about old age is I don't know any better. 2012
02-25-2011 #11
Registered User
- Join Date
- Jan 2010
- Location
- Elk River, MN
- Posts
- 676
Roger that dontlift, just give me a shout if you need any small stuff, our laser guy likes helping out with personal stuff.
Looks sharp JRouche, very nice work! The first 2 pics aren't showing, so forgive me if it's shown there, but how did you make the cut on yours? I've been mentally trying to figure out how a guy with a drill press could make a part like that, but the more I think about it, the more I think it'd need to be done on a mill with the table locked down for each hole.
-mattMatt Peterson 84 Monte Carlo - Sold :( | 99 Corvette Racecar | 2001 Z06 Daily Driver
https://www.pro-touring.com/showthre...ng-Bertha-Back
http://ls1tech.com/forums/conversions-hybrids/1499192-84-monte-5-3-build.html
https://www.pro-touring.com/threads/...rvette-Racecar
02-25-2011 #12
Registered User
- Join Date
- Nov 2008
- Location
- So. Cal.
- Posts
- 1,240
Hey Matt. I just marked the drill spots with a punch and drilled a pilot hole then stepped it up to a 3/8" bit then to another bit just under 3/4". I forget, it was prolly the 47/64th bit, maybe the 23/32nd drill bit, not sure. I have two silver and deming sets that are in 64ths so what ever was handy and as close to the reamer I had, adjustable reamer. I wanted the hole as close to the reamer size as possible, I hate chatter. And the reamer went in the drill press also. Originally Posted by monteboy84
The drill press is a heavy 20" clausing with auto feed and a magnetic base chuck (my introduction). It holds the parts just fine for simple drilling. No movement with a small 47/64th bit.
The reamer was pretty smooth also, even being a cheap strait reamer. Some good fluid helped. I like castrol moly-dee for the difficult stuff. I usually only use the moly-dee for stainless drilling and tapping. But its great for reaming also in mild steel. And really, I have a gallon of it so I use it were there might be any burnishing of the cutter due to speed, SFPM, like a large drill bit or reamer.
It sounds crazy that a fluid could make that much of a diff. But the moly-dee does make a diff. Its the difference between cutting the hole or chattering yer way through a hole and ruining the cutter in the process.
I love it for stainless steel. But it is a dream when cutting mild steel with a reamer also. If you havent used it you wont get it. I have used so many cutting fluids. But the moly-dee is king as far as I am concerned. Yup, it reaks big time, nasty stuff. But really, it has proven its ability to reduce all chatter.
Not to mention working stainless steel. I have ruined more drill bits than I care to say before I got the moly-dee. Stainless can be a bitch to machine, even drill through. The moly-dee is a wounder fluid. Makes machining hard stainless a breeze.
But really, I have two CNC mills, they are both small, the larger one is the Bridgeport and by the time I got on the computer to map it all out I was able to get it done. Im faster with the machines then I am with the computer. And my drill press has just as much power as my mill does. So powering through the holes was not an issue.
I dont know. Some times I just like to keep it simple. JRWhat I write is opinion, none of it is factual. 2010
Even though I'm conscious it doesn't mean I'm coherent. 2011
I'm getting better with age. Best thing about old age is I don't know any better. 2012
02-27-2011 #13
Registered User
- Join Date
- Jan 2010
- Location
- Elk River, MN
- Posts
- 676
Cool, thanks for the info. I do a bit of light gunsmith work, and always end up ruining drill bits on hard material, especially stainless, so I'll be sure to give that fluid a try. Tips like that are priceless, as with most of this stuff there is really no way to know without talking to someone who's been there, or to just dive in blind on your own.
-mattMatt Peterson 84 Monte Carlo - Sold :( | 99 Corvette Racecar | 2001 Z06 Daily Driver
https://www.pro-touring.com/showthre...ng-Bertha-Back
http://ls1tech.com/forums/conversions-hybrids/1499192-84-monte-5-3-build.html
https://www.pro-touring.com/threads/...rvette-Racecar

 Reply With Quote



