


Results 1 to 13 of 13
Thread: Metal band saw conversion
-
10-03-2006 #1

 Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435

Metal band saw conversion
I know that there have been a few post on here about this, but I was looking to see if somebody could help me with the math. I have a Delta 14" band saw in which the motor runs at 1725 RPM's. This goes into a 2.75" & 6" pully setup and then runs straight into the 14" wheels that run the blade. I am wanting to slow this thing down to a workable steel speed. If anyone with experience in this could help me with what size new pullies I need that would be cool. Thank you. Phillip
-
10-08-2006 #2 Registered User
- Join Date
- Aug 2001
- Location
- Connecticut
- Posts
- 1,571
I could bore you with the worksheets, but at our shop 250-500 ft per minute for metal work, you can get away with faster for aluminum with a larger tooth blade. Most of the time the saw we have the steel blade on is set at 450ft/min with a 10/14 variable pitch blade. Is there a gear box anywhere or just the belt drive? If it is just the belt drive you are at 2895 ft/min, so you would need another 6:1 reduction or maybe a little more.
1968 Camaro RS/SS, LS7 with Katech mods, T56 Magnum, C6Z06 Brakes
1968 Camaro RS Convertible LS3/480hp/4L70E
1962 Corvette 327-340hp stock
1963 Corvette Split Window Coupe
1967 Corvette L79 convertible
2006 Corvette Z06
2011 Corvette GS convertible
10-16-2006 #3
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
No it is just the belt drive. I wish that I would have seen this post earlier because i am almost done with the jack shaft. I am now coming out of the motor with a 2" into a 9"/2" jack shaft and into another 9" on the saw. This should then put me in the low 300's and that should be okay actually.
10-29-2006 #4
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
Just wanted to give you guys an update on my bandsaw. The jackshaft was pretty easy to build but was time consuming to try and come up with the design. Here are a couple of shots.
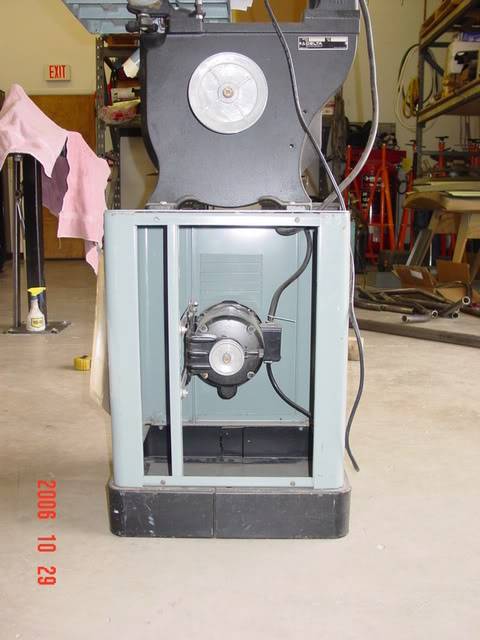
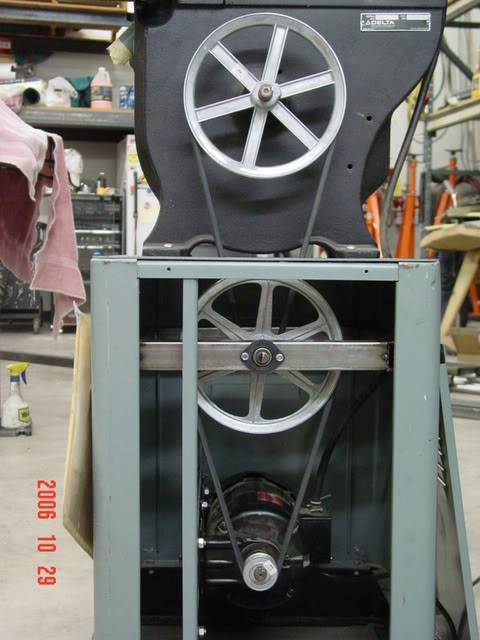
So in the end I have under a $100 in this project, thanks to my grandfather for giving me the saw .
10-30-2006 #5 Registered User
- Join Date
- Jul 2003
- Location
- allen, texas
- Posts
- 229
where did the parts come from? i could use some recources
10-31-2006 #6
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
All of the pullies came from my local Ace hardware, and the two needle bearings i bought online for 7.50 each. Be sure to get the self aligning bearings though, it makes it much easier when building the rig if you can be off up to 5 degrees on the alignment. I just googled bearings and found a website that offered self aligning needle bearings with a mounting surface attached to it. The steel is just 1.5 in. box. (.083 wall I think) -Phillip
10-31-2006 #7
Registered User
- Join Date
- Aug 2004
- Posts
- 540
Low 300's is still a bit fast -- blade wear is probably going to be a problem.
Ideally you need to be about half that.
10-31-2006 #8
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
I keep getting differing opinions about optimum speed. Its really not a big deal to me because I can easily change the pulley sizes, I am just tring to get a concensus on speed and tooth count on the blade. The other problem is what are people cutting? I plan to be cutting 18g. sheet metal.
11-01-2006 #9
Registered User
- Join Date
- Aug 2004
- Posts
- 540
Low 300's should work for thick aluminum with a 14/16 blade.
I am running around 120-150 with a 32T when cutting 18gage and it works perfect.
11-01-2006 #10
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
2 questions, 32T? is this a 32 tooth per in. blade? and second, the slowest I can get mine down to with only 1 jack shaft is going to be around 160-170 this should be close enough i would think?
11-01-2006 #11
Registered User
- Join Date
- Aug 2001
- Location
- Connecticut
- Posts
- 1,571
I think you'll be fine- one of our saws at work has a digital FPM meter on it and I can't recall ever seeing it below 200. Just make sure you get a really good quality bimetal blade (such as Starrett)- you can run them faster safely compared to a cheapo carbon steel blade.
1968 Camaro RS/SS, LS7 with Katech mods, T56 Magnum, C6Z06 Brakes
1968 Camaro RS Convertible LS3/480hp/4L70E
1962 Corvette 327-340hp stock
1963 Corvette Split Window Coupe
1967 Corvette L79 convertible
2006 Corvette Z06
2011 Corvette GS convertible
11-01-2006 #12 Registered User
- Join Date
- Mar 2003
- Location
- Fallston, MD
- Posts
- 564
Blades are identified by teeth per inch. Originally Posted by PhillipM
Brian Schein
11-03-2006 #13
Registered User
- Join Date
- May 2001
- Location
- Mesa, Az.
- Posts
- 1,435
Thanks for the info. I think that I will regear it a little bit more to get it closer.

 Reply With Quote



